Choosing between passivation and a conversion coating is one of the most consequential decisions in stainless steel finishing. Both treatments are applied after fabrication, both are described as "corrosion protection", and both are frequently quoted at similar prices — yet they work on completely different principles, and specifying the wrong one is a reliable route to failed test results and field complaints. This guide breaks down how each chemistry behaves on austenitic stainless steel, where the trade-offs sit, and how to pick the right post-treatment for a specific workpiece and end use.
The core difference in one paragraph
Passivation removes. A conversion coating adds.
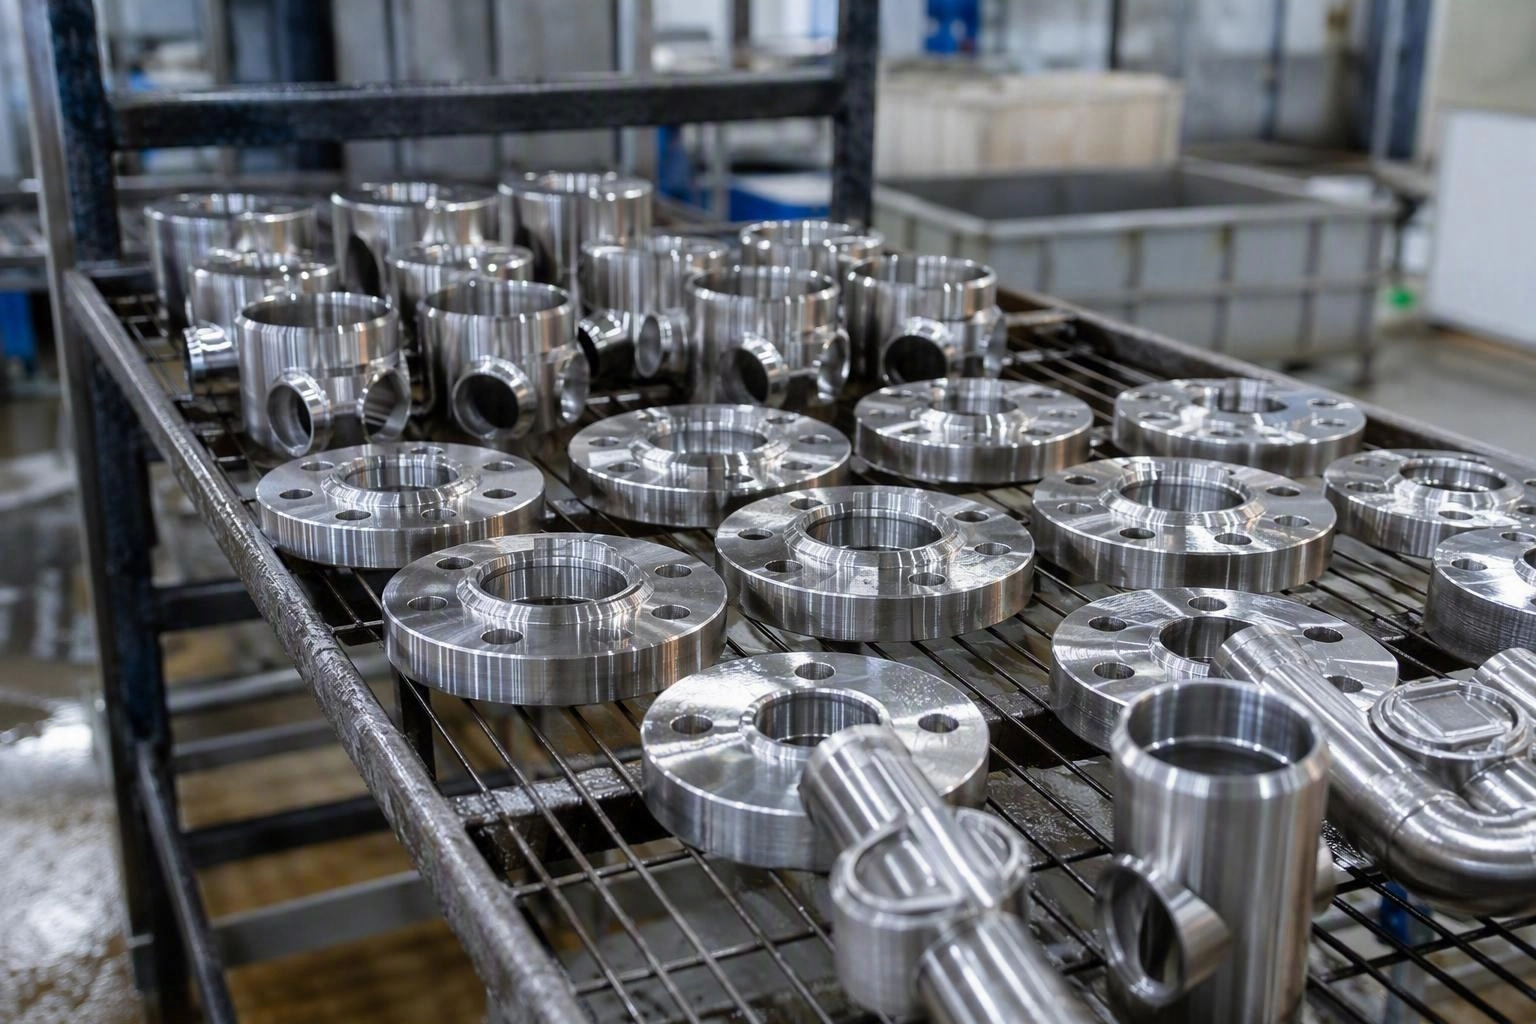
Passivation is a chemical cleaning and stabilization process. It dissolves the free iron, embedded tool steel, and surface contaminants left behind by machining, forming, and welding, and encourages the naturally protective chromium oxide layer on the stainless steel to re-form uniformly. The part does not gain a new layer of material — it loses the things that were preventing its own oxide layer from working.
A conversion coating deliberately builds a new inorganic film on the surface. In stainless steel service this usually means a ceramicizing or silane-based treatment that creates a thin, dense, chemically bonded layer with its own barrier properties, on top of whatever the base metal already offers.
That single distinction — subtractive versus additive — drives almost every practical difference that follows.
What each treatment actually does
| Dimension | Passivation | Conversion coating |
|---|---|---|
| Mechanism | Dissolves free iron and contaminants; rebuilds the native chromium oxide layer | Deposits a new inorganic film bonded to the metal surface |
| Dimensional effect | None measurable; no material added | Nano to micron scale film; still negligible for most tolerances |
| Typical bath | Acidic, oxidizing or organic-acid based | Silane, ceramic, or zirconium/titanium based |
| Primary purpose | Restore inherent corrosion resistance; remove weld heat tint contamination | Add barrier protection; improve adhesion for subsequent coatings |
| Effect on appearance | Bright, metallic, essentially unchanged | Usually slight colour or sheen shift, occasionally a faint iridescent tint |
| Conductivity | Preserved | May be affected depending on film chemistry |
| Typical service life of effect | Long-term, integral to the metal | Depends on film durability under abrasion and chemical exposure |
When passivation is the right answer
Passivation is the default choice for austenitic grades — 304, 304L, 316, 316L, 321 — whenever the goal is to make the stainless steel behave the way the mill certificate says it should. Specific situations where it is clearly correct:
- After welding. Welding burns chromium and leaves heat tint, oxide scale, and often free iron from the filler or adjacent carbon steel tooling. Passivation (usually after a dedicated pickling or descaling step) restores the chromium-depleted zone.
- After machining and forming. Cutting tools embed iron particles into the surface. These particles rust, and the rust stains the surrounding stainless steel. Passivation removes them.
- Food, beverage, pharmaceutical, and medical equipment. These industries care about a clean, non-shedding, chemically inert surface. Adding an organic or ceramic film is usually unwanted, and in some cases non-compliant with hygiene standards.
- Parts that must remain electrically conductive — busbars, connectors, shielding.
- When the part will be electropolished or further chemically processed. A residual conversion film interferes with the next step.
For these cases, a two-in-one product such as LG303 Stainless Steel Two-in-One Passivation Agent is often the practical choice. It combines acidic degreasing (activation) and chemical passivation in one immersion step, which removes the separate alkaline degrease stage and shortens the line. LG303 contains no nitric acid, hydrofluoric acid, or hexavalent chromium, works at room temperature to 50 °C with a 5–15 minute soak, and is formulated for 300-series stainless steel. On a normal workload it passes both the blue dot (potassium ferricyanide) test and standard salt spray requirements.
When a conversion coating makes more sense
Conversion coatings earn their place when the requirement goes beyond restoring the base metal:
- You need extra corrosion margin. If the part faces aggressive chloride exposure, coastal service, or extended salt spray targets beyond what the base grade delivers, a ceramic or silane film adds a genuine barrier layer.
- The part is a mixed-material assembly. Where stainless steel sits alongside aluminium or carbon steel, a conversion film can reduce galvanic risk and give the whole assembly a consistent surface.
- You need a paint, powder, or adhesive to stick. Conversion coatings are established adhesion promoters. Passivation does not improve adhesion — it leaves a passive oxide that paint struggles to key into.
- Scratch and fingerprint resistance matters. Ceramicizing agents such as LG909 Ceramicizing Agent create a hard, low-energy surface that resists handling marks and makes subsequent cleaning easier.
- You are moving away from hexavalent chromium. Chrome-free passivation such as LG908 Chrome-Free Passivation Agent is frequently specified as a drop-in replacement where a chromium-based process is being phased out, providing a conversion-type film without the restricted substance.
Process considerations that change the answer
Chemistry is only half the decision. Three process realities usually settle it:
1. Line length and available stages. Passivation is typically a shorter sequence: pre-clean, passivate, rinse, dry. A conversion coating usually needs tighter control of the preceding cleaning stage, because the film cannot form over oil or oxide. If the shop has limited tank space, passivation is often cheaper to run.
2. Water quality. Both processes are sensitive to rinse water, but conversion coatings are less forgiving — dissolved solids and residual hardness in the final rinse show up as streaking and uneven film. If deionised or RO water is not available, passivation is more robust.
3. What the customer will actually test. Ask this explicitly rather than assuming. If the acceptance criterion is a blue dot test, passivation is what is being asked for. If it is a salt spray hour count on a coated assembly, the answer is usually a conversion coating plus the topcoat.
A practical decision sequence
- Confirm the base material and grade. Passivation requirements for 304 and 316 are well established; free-cutting grades with high sulphur or copper content behave differently and need to be checked before treatment.
- Identify the contamination. Light oil, fingerprints, and thin films can often be handled in a single two-in-one step. Heavy grease, polishing paste, and thick oxide scale require conventional pre-cleaning first — this is not optional, because oil left on the surface blocks the passivation reaction underneath it.
- Decide whether something must be added to the surface or removed from it. If nothing needs to be added, do not add it.
- Check downstream steps. Painting, bonding, and electropolishing push strongly toward one option.
- Test on real parts, not coupons, before committing a production bath.
Common mistakes worth avoiding
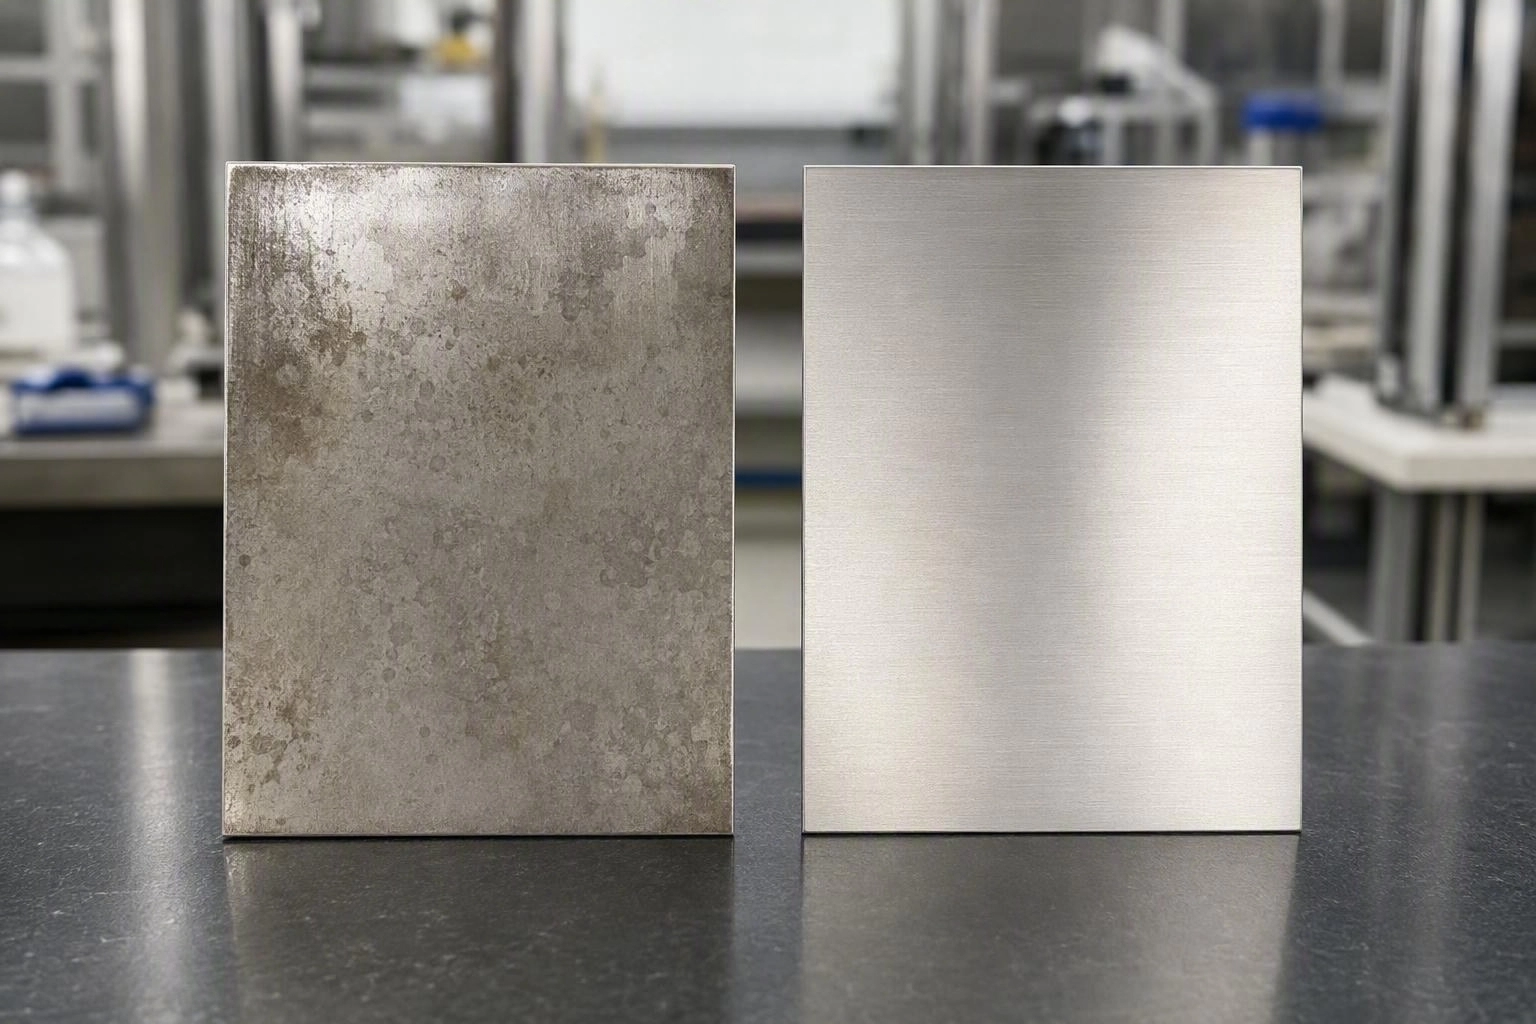
The two most expensive errors we see are not chemistry errors at all. The first is skipping adequate pre-treatment: treating a visibly oily workpiece with a passivation bath leaves the oil film intact and produces a part that looks treated but fails in service. Heavy oil, polishing compound, or grease must be removed with an alkaline degreaser and fully rinsed until the surface holds a continuous water film.
The second is inadequate rinsing after treatment. Residual chemical left in crevices and weld seams is one of the most frequent causes of subsequent pitting and discolouration — and it is often mistaken for a product failure rather than a rinse failure.
Where to start
If you are treating 300-series stainless steel and the goal is restoring inherent corrosion resistance, a two-in-one passivation agent is usually the most efficient route. If you need additional barrier performance, adhesion for a coating, or a chrome-free replacement for an existing process, a conversion-type product is the better fit. Many production lines we support eventually run both, in different corners of the shop, for different part families.
Foshan Changcheng Surface Technology produces passivation agents, chrome-free passivation agents, ceramicizing agents, silane sealants, and a full range of associated cleaning chemistry. We are happy to review your workpiece, substrate, and test requirements and recommend a starting point — or send a sample for your own line trial. Technical datasheets, ISO / MSDS / RoHS documentation, and electronic catalogues are available on request.