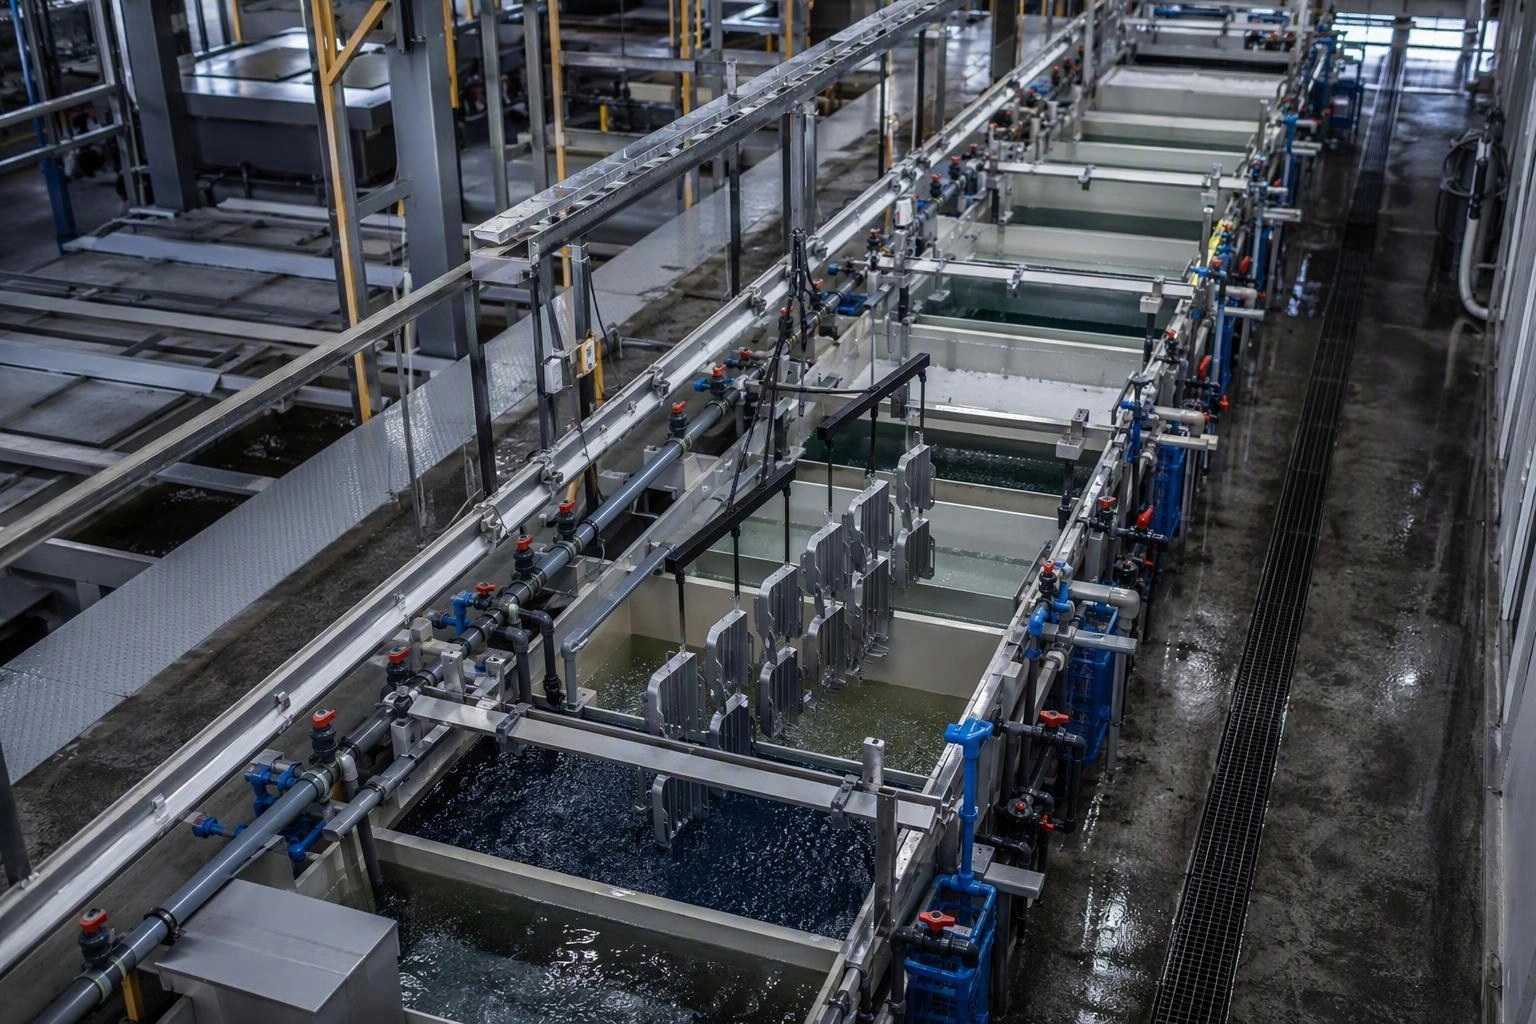
Zinc phosphating and silane pretreatment occupy the same slot in a finishing line: the stage between cleaning and the final coating or corrosion protection step. Both create a conversion layer on steel and aluminium. Both improve adhesion and corrosion performance. But they behave very differently in operation, and the choice has real consequences for bath control, waste treatment, line length, and the range of materials a single line can process.
How each process works
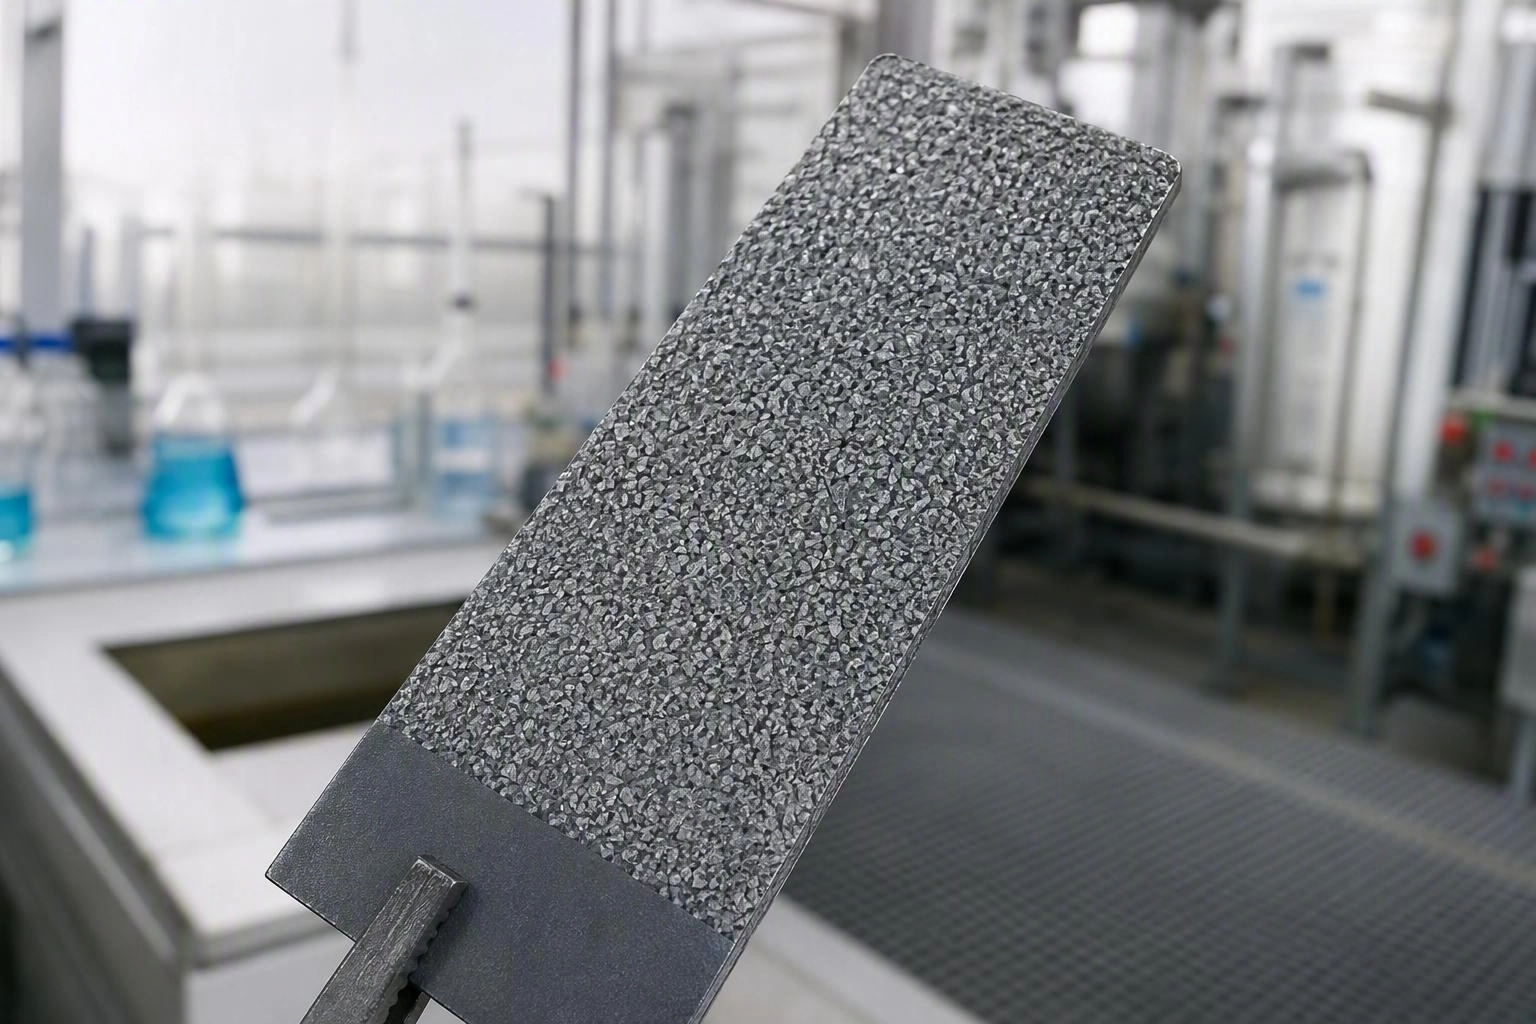
Zinc phosphating attacks the metal surface with an acidic solution containing zinc and phosphate. The acid dissolves a small amount of base metal, the local pH rises at the surface, and insoluble zinc phosphate crystals precipitate and grow into a dense, grey, crystalline layer. That layer is porous — deliberately so. It provides a mechanical key for paint and an additional barrier to corrosion, and the crystal structure is thick enough to be visible under magnification.
Silane pretreatment works through hydrolysis and condensation. Organofunctional silanes in an aqueous bath form silanol groups that hydrogen-bond to hydroxyl groups on the metal surface, then cross-link on drying into a thin, dense, largely inorganic film. It is not a crystalline deposit. It is more like a chemically bonded molecular layer, typically measured in nanometres rather than microns.
Head-to-head comparison
| Factor | Zinc phosphating | Silane pretreatment |
|---|---|---|
| Film thickness | 1–5 µm typical (crystalline) | Nanometre scale (molecular) |
| Bath stages | Usually 4–6 incl. activation, rinse, passivation rinse | Typically 2–3 |
| Operating temperature | Often 35–55 °C; some low-temperature variants | Frequently room temperature |
| Multi-metal capability | Steel-focused; aluminium and galvanised need separate formulations | Steel and aluminium in the same bath |
| Sludge generation | Significant; requires regular desludging | Minimal |
| Wastewater load | Heavy metals, phosphate; costly to treat | Substantially lower |
| Adhesion for paint | Excellent, well-established | Excellent, often better on aluminium |
| Salt spray performance | Strong, especially under powder coat | Comparable on many systems, formulation dependent |
| Process control complexity | Higher — free acid, total acid, accelerator, temperature | Lower — mainly pH and concentration |
| Typical sectors | Automotive, appliances, heavy steel | Aluminium profiles, mixed-metal assembly, appliance |
Where zinc phosphating still wins
- Heavy steel structures under powder coat or wet paint. The crystalline layer gives a mechanical key that performs reliably under impact and bending.
- Long-established specifications. Automotive OEM specifications frequently name phosphating explicitly. Changing a qualified process requires re-validation, which is expensive.
- Parts with residual surface variability. The phosphating reaction is somewhat self-correcting on mildly inconsistent steel, whereas a silane film demands a genuinely clean, uniformly active surface.
- Operations that already handle phosphate sludge and wastewater. If the treatment plant exists and is permitted, the incremental cost of phosphating is lower.
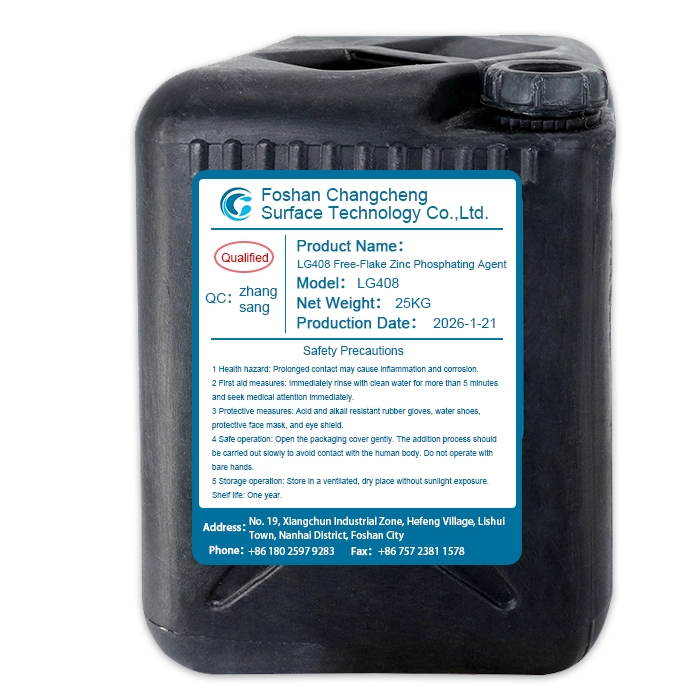
For these cases, a modern phosphating line benefits from tight process discipline. LG408 Free-Flake Zinc Phosphating Agent, for example, is formulated to control crystal growth so the coating adheres as a fine, uniform layer rather than loose flake, which is a common cause of coating defects and dust in the tank.
Where silane pretreatment wins
- Mixed steel and aluminium production. One bath, one set of parameters, both substrates. This is the single strongest argument for silane in job shops and appliance plants running multiple materials.
- Environmental and permit pressure. No phosphate, no heavy metals, dramatically less sludge. Sites facing discharge limits often move to silane simply to stay compliant without building a larger wastewater plant.
- Shorter lines and lower energy bills. Fewer stages and room-temperature operation reduce both capex and running cost.
- Aluminium-dominant work. On aluminium, silane films frequently outperform phosphating for adhesion and give a more consistent appearance.
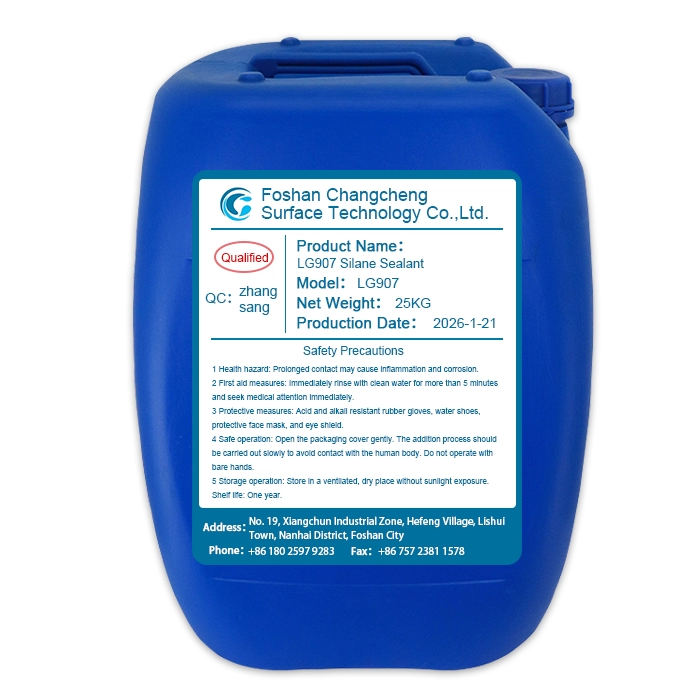
LG907 Silane Sealant is representative of this family: it builds a dense organosilane film through a simple room-temperature immersion, with no sludge generation and a minimal rinse requirement. Where a line needs to handle both steel and aluminium without duplicating tanks, or where a formulator wants a phosphate-free route to adhesion, silane is usually the more practical answer.
The transition stage that gets overlooked
One practical point decides the outcome more often than the chemistry itself: what happens to the surface between cleaning and the pretreatment bath.
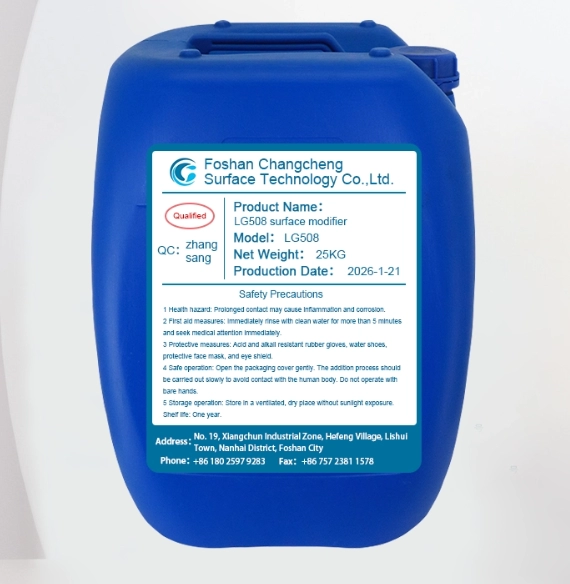
If parts flash-rust after the cleaning rinse and before entering the phosphating or silane tank, film quality collapses. On steel this is a very common defect. The usual fixes are a short inter-stage rinse with a mild rust-preventive additive, or a surface modifier stage that keeps the surface active and wettable while it waits. Products such as LG508 surface modifier exist for exactly this purpose — not as a treatment in their own right, but as a stabiliser for the transition.
Silane baths are less tolerant of this than phosphating baths. A phosphating bath can partly cope with light surface oxidation because it dissolves base metal as part of the reaction. A silane bath cannot. If your line has long transfer times or parts sit in a rack between stages, plan for that explicitly.
Control parameters to monitor
Regardless of route, four parameters determine whether the process stays in control:
- Cleaning quality. Both processes fail over residual oil. Verify with a water-break test — the surface should hold a continuous, unbroken water film. If it beads, the pretreatment stage is being asked to do the cleaner's job and will not succeed.
- Bath concentration and pH. Phosphating needs free acid, total acid, and often accelerator titration. Silane needs pH and solids content. Neither tolerates guesswork.
- Temperature. Phosphating is temperature-sensitive; a drop of a few degrees slows crystal growth noticeably. Silane is far more forgiving but still benefits from stability.
- Rinse quality. The final rinse before drying must be clean. Dissolved solids in that rinse become the defects you see after curing.
Choosing between them
If your line processes mostly carbon steel, your customer specification names phosphating, and you already operate a wastewater plant, stay with phosphating and focus on crystal control and sludge management. If you process aluminium, or mix aluminium and steel, or you are under pressure to cut sludge and discharge, silane pretreatment is normally the better long-term investment — at the cost of accepting a slightly narrower margin for cleaning errors.
Foshan Changcheng Surface Technology supplies both routes, along with the degreasers, surface modifiers, and rust preventives that surround them. Send us your substrate mix, current line stages, and coating specification, and we will confirm which route fits — or provide samples for a side-by-side trial on your own parts.