Lead time is one of the least transparent parts of buying metal surface treatment chemicals. A quoted figure of "15 to 30 days" is accurate for a large share of orders, but it is not a fixed property of a product — it depends on whether the item is a stock model or a custom formulation, whether a sample has been tested and approved, and how quickly the specification is confirmed. This article explains what actually determines the timeline, so buyers can plan around it rather than guess.
The two paths: stock models and custom formulations
| Stock model | Custom / OEM formulation | |
|---|---|---|
| Typical lead time | Days, subject to available stock | Usually 15–30 days after specification confirmation |
| Prerequisite | Order confirmation | Confirmed specification plus approved sample |
| Sample stage | Not required, or optional | Required — this is where most of the elapsed time sits |
| Minimum order | Low | Higher, reflecting batch economics |
| Documentation | Available for the standard product | Prepared against the final formulation |
| Main risk to schedule | Stock availability at order time | Line trial outcome and specification changes |
Where the same formulation is already produced as a standard catalogue item, or where an existing formulation can be supplied under a customer's brand, lead time is dominated by stock and logistics. Custom development is a different process with different timing, and it is worth understanding the stages before committing.
Stage 1: Requirement capture
Before any formulation work begins, we need the technical parameters that determine what the product has to do:
- Substrate and grade
- Contamination type and loading
- Process method — immersion, spray, or manual
- Available operating temperature
- Treated surface area per shift
- Rinse water quality
- The acceptance test and pass threshold
- Existing line stages, before and after the target stage
This stage costs the customer nothing but is where timelines are won or lost. An enquiry that arrives without these details generates a round of clarification that can add days. An enquiry that includes them permits a specific product recommendation in the first response.
Stage 2: Recommendation and sample
Our first substantive answer will normally be a recommendation with a rationale: either a standard product that fits, or a statement that the requirement falls outside the standard range and requires development.
Where a standard product fits — which is the majority of enquiries — the next step is a sample for trial on the customer's own parts. This is the single most valuable stage in the process, and it is deliberately cheap. A trial on real parts in real conditions resolves questions that no datasheet can answer, and it prevents the far more expensive outcome of discovering a product mismatch after a production-scale order.
What we need from the customer for a meaningful trial
| Item | Why |
|---|---|
| Sample quantity of the actual parts | Real geometry, real soil, real surface condition |
| Existing process parameters | Trial must reflect what the line can actually do |
| Available rinse water | Rinse quality frequently determines the outcome |
| The acceptance test and threshold | Otherwise the result cannot be judged |
| Line constraints | Tank volume, handling equipment, temperature limits |
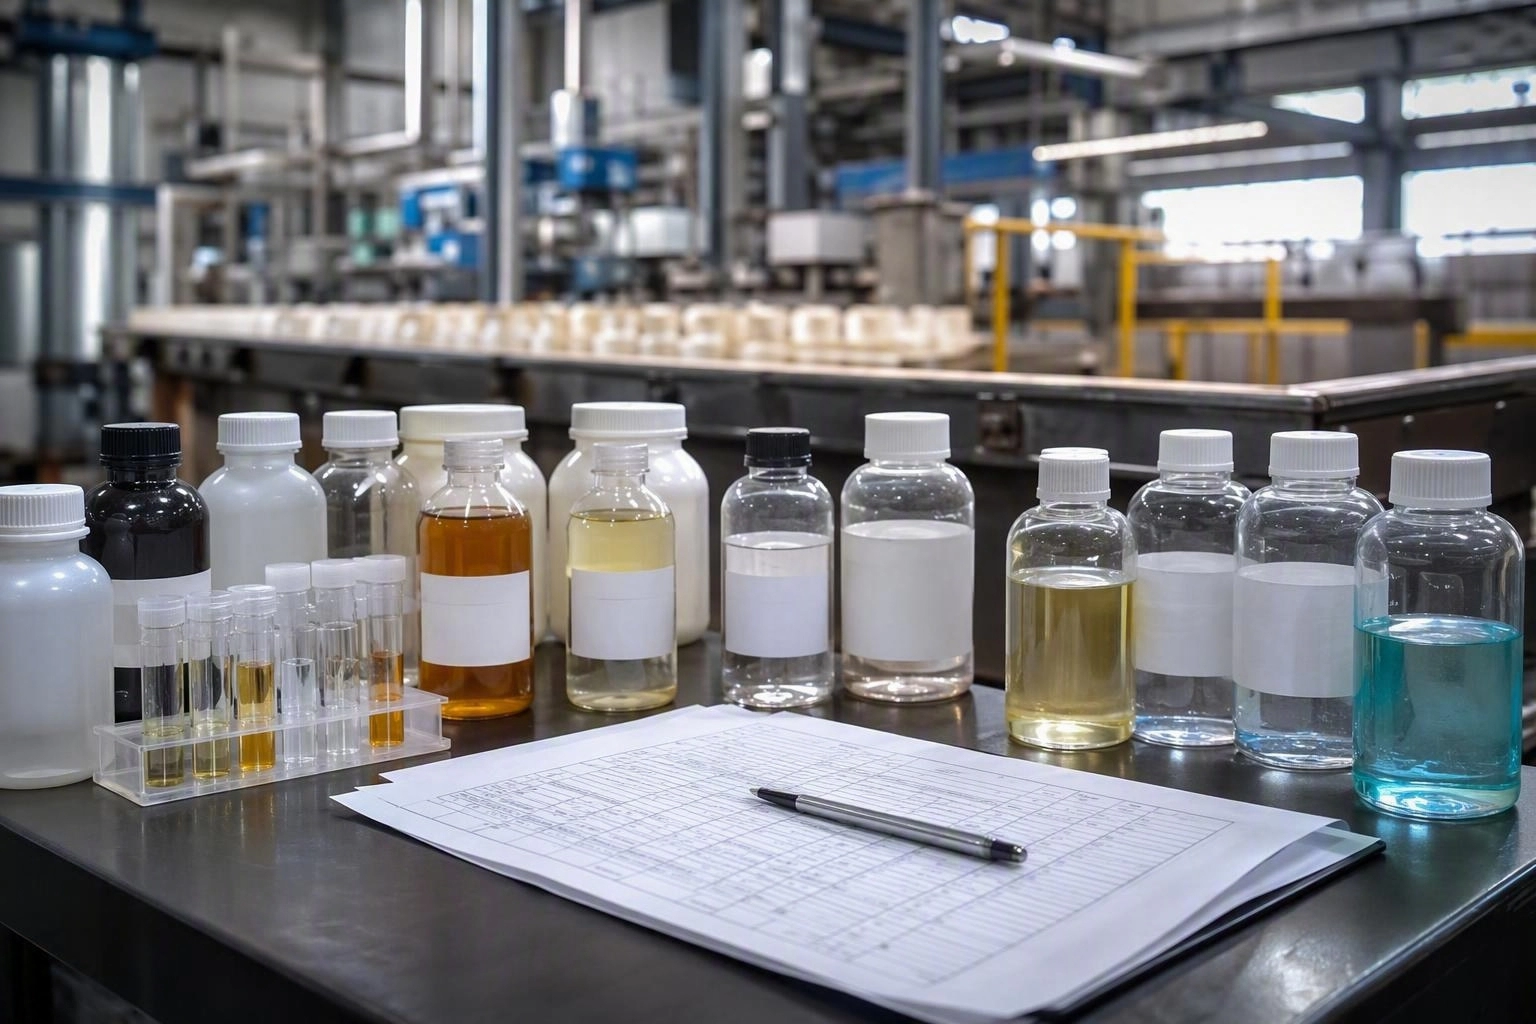
A trial conducted on coupons in our laboratory tells us the chemistry works in principle. A trial conducted on the customer's parts, in the customer's line, with the customer's water, tells us whether it will work in production. These are not the same test, and we treat the second as the meaningful one.
Stage 3: Line trial and parameter setting
Once a sample is in the customer's hands, three outcomes are possible:
- The standard product works as supplied. The most common outcome. Parameters are confirmed and the order can proceed on a stock or light-customisation basis.
- The product works with process adjustments. Concentration, time, temperature, or rinse conditions need tuning. Still a standard product, and usually resolvable within days.
- The product does not work. This indicates the requirement is genuinely outside the standard range, and triggers the custom development route — with a clear technical target, because we now know exactly what the standard product failed to achieve.
Being explicit about which outcome occurred is what makes the timeline predictable. The riskiest situation in this industry is an ambiguous trial result that neither clearly passes nor clearly fails, because it leads to repeated trials with no defined endpoint. Defining the acceptance test and threshold at the requirement-capture stage prevents that.
Stage 4: Production and documentation
Once the specification is confirmed and any sample approved, the remaining lead time is production, packaging, and documentation:
| Activity | Notes |
|---|---|
| Production batch scheduling | Stock items ship from available inventory; custom items are scheduled into a production run |
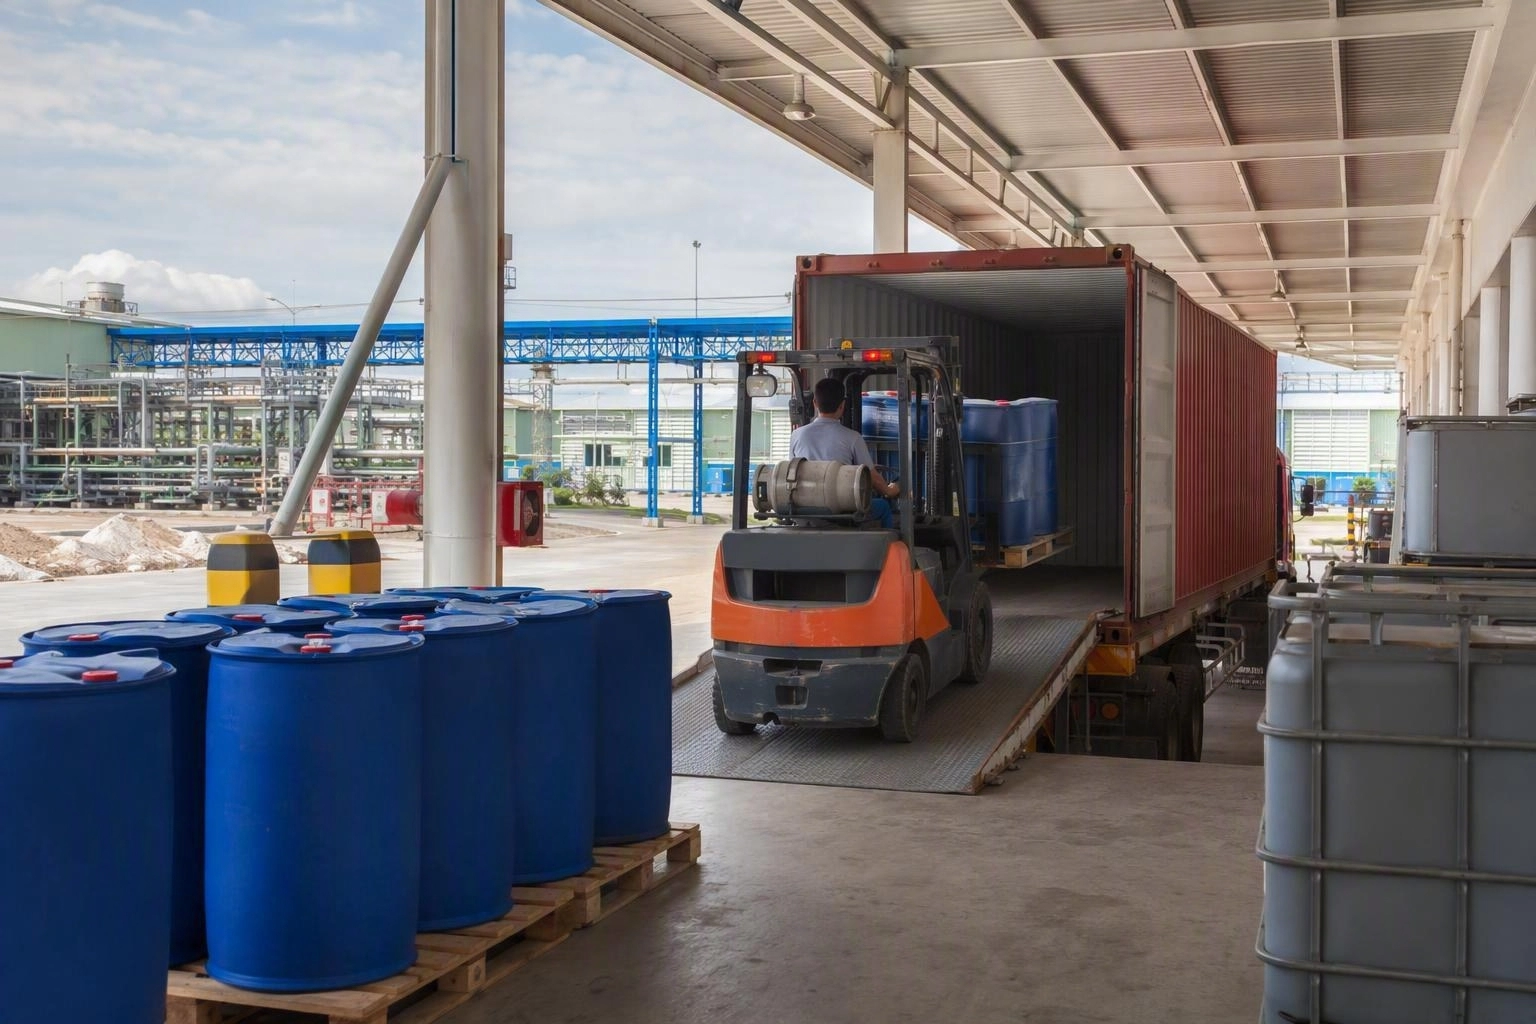
| Packaging | 25 kg plastic drums and 1000 kg plastic drums are standard; other formats on request |
| Quality documentation | Batch records and specification confirmation against the approved sample |
| Compliance documentation | MSDS, ISO and RoHS documentation in the required language |
| Export documentation | Commercial invoice, packing list, certificate of origin as applicable |
| Shipping arrangement | Air, sea, or express; trade terms FOB, CIF, or DDP |
The stated 15–30 day window applies from confirmed specification to shipment, and it can extend during peak seasons or when special materials are required. We would rather state that clearly upfront than let a customer plan a production launch around an optimistic figure.
Practical measures that shorten the timeline
- Send the nine technical parameters with the first enquiry. Substrate, soil, method, temperature, area, water quality, acceptance test, line stages, packaging and documentation needs. This removes the most common source of delay.
- Identify whether a standard product is acceptable before requesting custom development. Most requirements are met by the standard range.
- Prepare parts and line time for the trial before the sample arrives. Samples that sit in a warehouse waiting for a production window add weeks.
- Define the acceptance test precisely. "Better corrosion resistance" is not a test. "Blue dot test, no blue within 30 seconds" is.
- Confirm documentation requirements early. MSDS and compliance documents in a specific language can be prepared in parallel with production, but only if the requirement is known.
- Consider stock models for initial production. Where a standard product meets the requirement, starting with stock while a custom variant is developed keeps production running.
- Tell us about mixed-model orders. We welcome them, and they help customers reduce inventory pressure — but they need to be planned into the production schedule rather than added afterwards.
Working with us
Foshan Changcheng Surface Technology Co., Ltd. manufactures a full range of metal surface treatment chemistry for iron, aluminium, die-cast aluminium, galvanised, and magnesium-plated parts, serving hardware processing, machinery manufacturing, electronics, building materials, and automotive customers. Our product range includes alkaline and acidic degreasers, neutral cleaners, neutral rust removers, phosphating agents, conversion coating agents, chrome-free passivation agents, ceramicizing agents, silane sealants, surface modifiers, and demolding agents.
We hold stock of regular models, follow delivery schedules strictly, and accept mixed-model orders. ISO, MSDS, and RoHS documentation can be supplied as required, and electronic catalogues and product brochures are available on request. Send us your requirement and we will confirm whether a stock product fits or whether a custom formulation is needed — and give you a realistic timeline for either route.