Spray degreasing lines have a reputation for being difficult to keep in control, and the three symptoms that generate most complaints — persistent foaming, oil re-depositing on parts, and baths that have to be dumped far sooner than expected — are all connected. They are usually symptoms of one root problem: the bath is being asked to carry more oil than it can hold. This article explains the mechanisms and sets out a systematic fix.
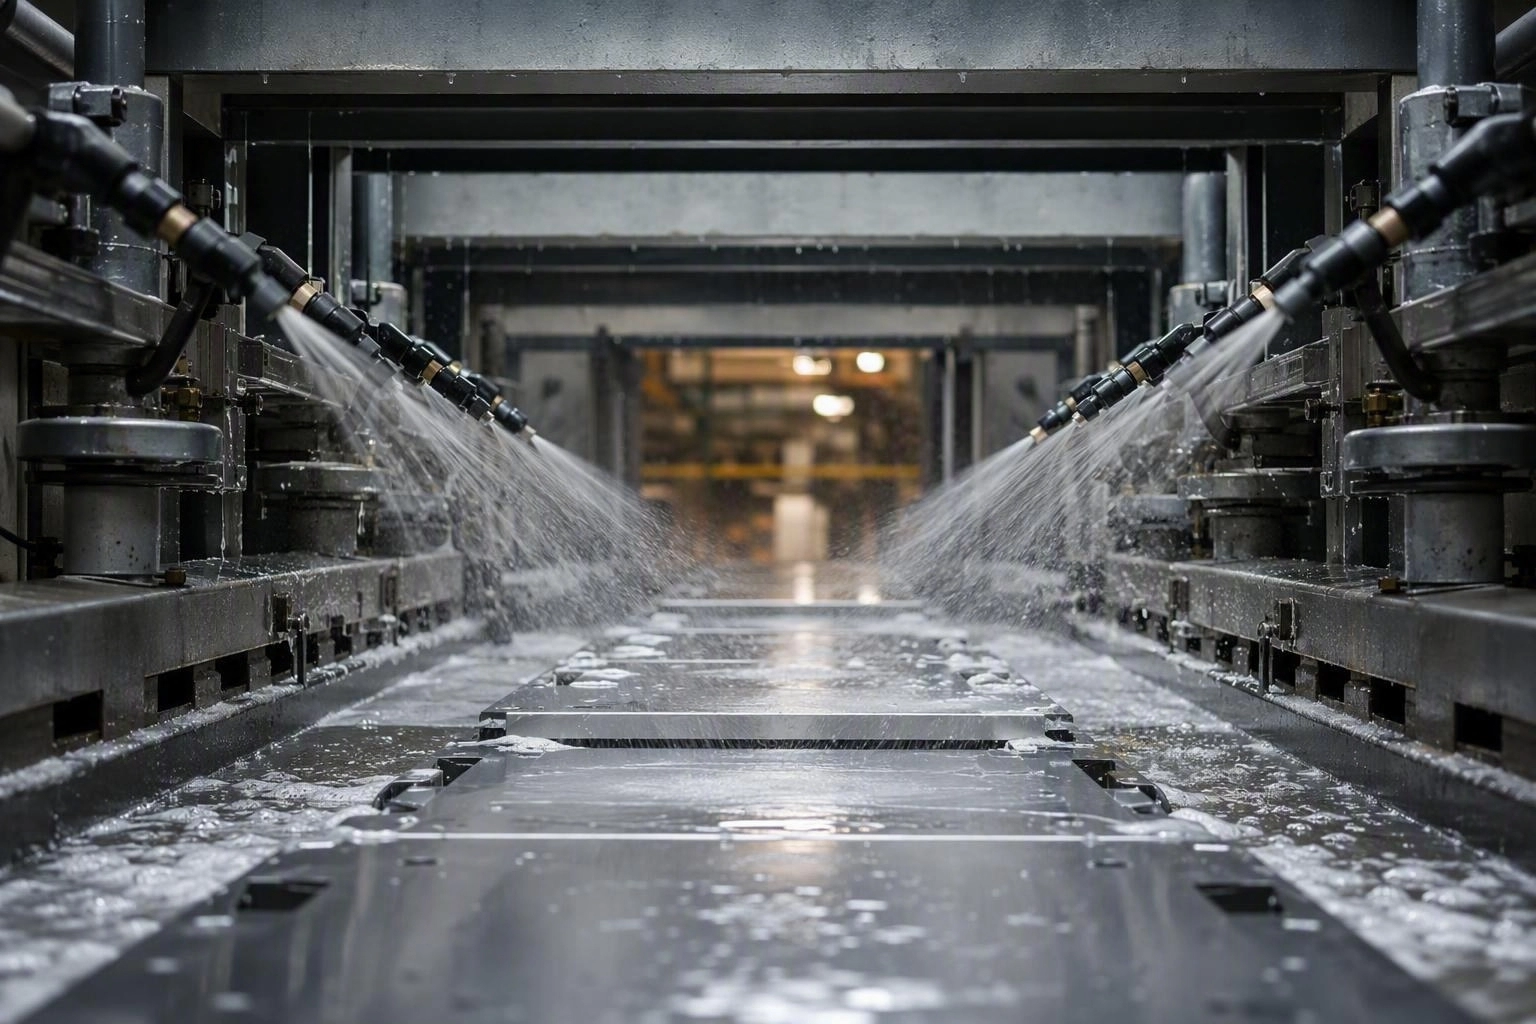
Understand the constraint first: spray is not immersion
The two processes impose fundamentally different chemistry requirements.
| Immersion | Spray | |
|---|---|---|
| Contact time | Minutes (3–15 typical) | Seconds (20–120 typical) |
| Mechanical action | Passive; relies on solution wetting | High; impingement force assists soil removal |
| Foam tolerance | Moderate | Very low — foam blocks nozzles and causes pump cavitation |
| Concentration tolerance | Broad | Narrow |
| Bath volume relative to throughput | Large | Small — contaminant concentration rises fast |
| Chemical consumption | Mostly drag-out and reactive depletion | Mostly drag-out plus overspray and mist loss |
The short contact time and small bath volume are the two facts that drive everything else. A spray bath receives the same oil load as an immersion bath processing similar throughput, but has far less volume to dilute it in, and far less time per part to remove it.
Symptom 1: Foaming
Foam in a spray line is not a cosmetic problem. In severe cases it overflows the tank, starves the circulation pump, blocks nozzles, and produces parts with untreated patches where spray coverage was lost.
Four causes, in order of frequency:
- Using an immersion-grade cleaner in a spray system. Immersion cleaners are frequently formulated with surfactants that generate and stabilise foam. This is the most common single cause. If the product datasheet specifies immersion only, do not put it in a spray line.
- Oil accumulation above the emulsification capacity. A cleaning bath has a finite capacity to hold emulsified oil. Once that capacity is exceeded, the surfactant system is consumed by the excess oil and loses its ability to control foam.
- Mechanical air entrainment. A leaking pump inlet, a low tank level allowing the pump to draw air, or a spray nozzle aimed at the liquid surface rather than the work all introduce air that manifests as foam.
- Carry-over of contamination from an upstream stage. Cleaning agents from a previous stage, or a high detergent load in the rinse, can destabilise the spray bath's foam profile.
The fix: Confirm the product is specified for spray application. Add or improve an oil separation mechanism — a skimmer, coalescer, or overflow weir, depending on the equipment. Check pump seals and tank level. Where the bath is genuinely overloaded, the answer is more frequent partial dumping, not more antifoam. Antifoam treatment suppresses the visible symptom while the oil load continues to rise, and it frequently causes defects of its own.
Symptom 2: Oil re-depositing on parts
Parts come out of a spray degreaser visibly oily, or appear clean then exhibit adhesion failures after coating. The mechanism is straightforward: the bath contains emulsified oil, and when the part is sprayed, some of that emulsion deposits back onto the surface. The dirtier the bath, the more oil goes back on the part.
This is the key insight that distinguishes a well-run line from a struggling one. A cleaning bath does not remain effective in proportion to the amount of oil it has absorbed — beyond a certain point, it becomes a net contaminant source.
Contributing factors:
- Bath oil load above the working limit. The primary factor. Every bath has a capacity, expressed either as a percentage of oil in the bath or as kilograms of oil per cubic metre, at which cleaning performance collapses.
- Insufficient mechanical oil removal. If the line has no skimmer or coalescing device, oil accumulates until the bath is dumped. With a proper separator, the bath can operate far closer to steady state.
- No rinse stage, or an inadequate one. Carry-over from the cleaner to the rinse to the next stage redistributes oil rather than removing it. Two-stage or counter-current rinsing is the standard remedy.
- Poor nozzle coverage. Blocked or worn nozzles leave parts of the workpiece untreated, which shows up as localised adhesion failure rather than general oiliness. Inspect nozzle performance regularly.
How to confirm: Take a water-break test on parts immediately after the final rinse. Beading indicates residual oil. Separately, measure the oil content of the bath itself — gravimetric extraction or a simple visual assessment of separated oil in a settled sample both give usable information.
The fix: Establish a measurable oil limit for the bath and enforce it. Install or repair the oil separation system. Improve rinsing. Where throughput has grown without a corresponding increase in bath volume, resize the bath or increase dump frequency — the original bath was specified for a lower load.
Symptom 3: Short bath life
A bath that needs dumping weekly instead of monthly is usually not a chemistry problem. It is a symptom of either an oil load beyond design capacity, or a bath management practice that lets contamination accumulate without control.
| Contributing factor | Effect on bath life | Remedy |
|---|---|---|
| Soil load exceeds design capacity | Directly shortens life; also causes foam and re-deposition | Resize bath, increase volume per part, or add a pre-clean stage |
| No oil separation | Bath acts as an accumulating oil reservoir | Skimmer, coalescer, or weir overflow |
| Replenishment by feel | Over-dosing then under-dosing; unstable performance and premature dump | Dose against measured concentration |
| Carry-over of upstream contamination | Consumes active chemistry prematurely | Improve pre-rinse; add a dedicated drag-out stage |
| Hard water make-up | Precipitates surfactants and builders out of solution | Soften or deionise make-up water |
| Temperature instability | Reduced reaction rate, requiring higher concentration for the same result | Stabilise heating control |
One additional factor deserves attention: bath stabilisation. In two-component systems, the additive component exists partly to buffer the working solution against impurity interference and harmful side reactions. LG706 Two-in-One Degreaser and LG707 Two-in-One Degreaser serve this role for their respective conversion coating partners, holding the working solution at its optimal process window and inhibiting the reactions that degrade the main bath. Where a line runs a two-component system, running with an incorrect or drifting component ratio is a common and entirely avoidable cause of short bath life — the fixed ratio is a process requirement, not a suggestion.
The two-in-one advantage in spray lines
For aluminium and steel spray pretreatment specifically, two-in-one chemistry offers a practical route to a more stable line. By combining degreasing and conversion coating in a single spray stage, the process removes the intermediate rinse that would otherwise redistribute oil, and shortens total line length.
Taking aluminium as an example: LG808 Aluminum Spray Acidic Degreasing Agent handles oil removal on aluminium in a spray application, while LG809 illuminant addresses the brightening requirement on the same substrate. Both are formulated with spray application in mind, which means low foam and short effective contact time — the appropriate design parameters for a line that measures contact time in seconds rather than minutes.
The equivalent route on steel is the LG406 / LG707 and LG407 / LG706 two-in-one pairs, which are designed to complete degreasing, oxide removal, and micro-film formation simultaneously in a high-speed spray system at pH 2.5–3.5, with a 2–4 minute effective spray time.
A line audit sequence
- Confirm product suitability. Verify that every chemistry in the spray stage is specified for spray application, not immersion.
- Measure the actual oil load in the cleaning bath and compare it against the supplier's stated working limit.
- Audit oil removal equipment. Skimmer, coalescer, weir — present, functioning, and sized correctly?
- Check mechanical factors. Pump seals, tank level, nozzle condition and pattern, spray pressure.
- Verify bath parameters against specification. Concentration, temperature, pH. In two-component systems, confirm the ratio between components.
- Test rinse effectiveness. Water-break test after the final rinse.
- Review make-up water. Hardness and dissolved solids.
- Review dump frequency against specification and establish a measurable trigger for dumping — oil content or treated area — instead of dumping on a fixed calendar with no reference to actual load.
Where to start
Foshan Changcheng Surface Technology supplies spray-suitable cleaning and pretreatment chemistry for steel and aluminium, including LG808 Aluminum Spray Acidic Degreasing Agent, LG809 illuminant, and the LG406/LG707 and LG407/LG706 two-in-one systems, along with the bath management guidance that goes with them. If you describe your line — material, throughput, tank volume, spray time, and the symptoms you are seeing — we will identify the most likely cause and recommend a product and parameter set. Technical datasheets, ISO / MSDS / RoHS documentation, and electronic catalogues are available on request.